
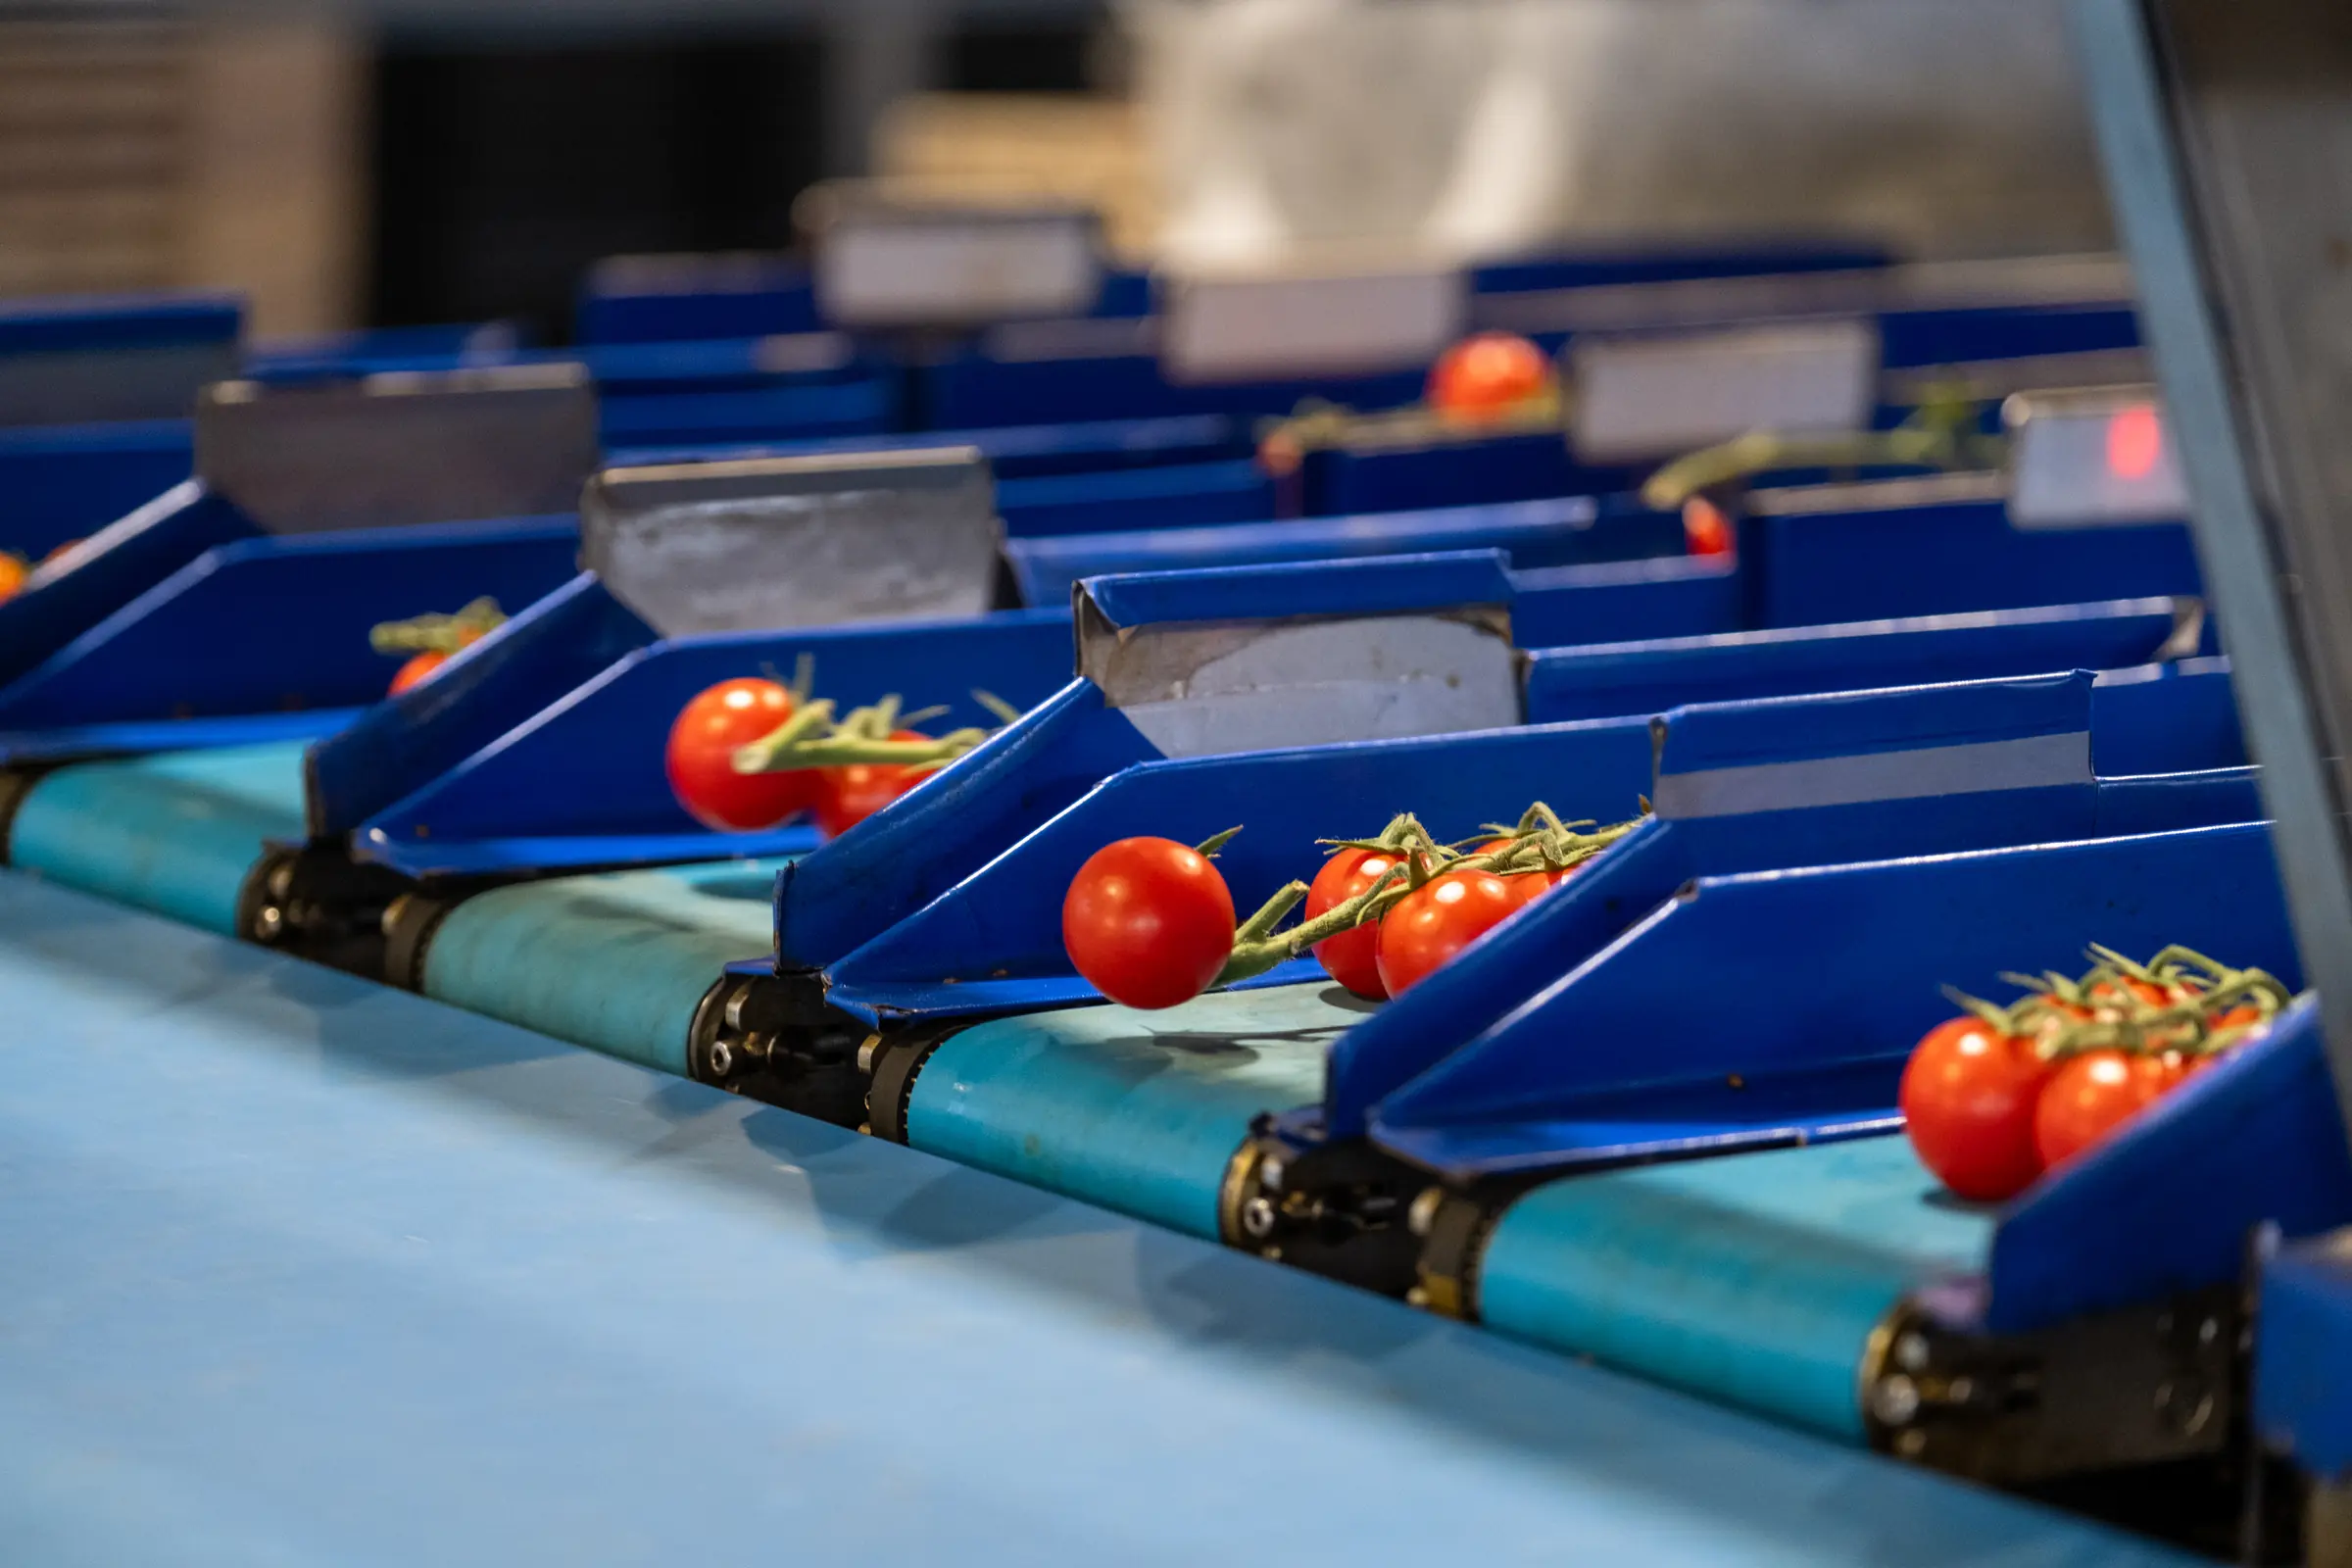
- The most costly fruit and vegetable packing house mistakes are often invisible at first: mixed batches, incorrect labels, out-of-tolerance weights, inconsistent grading and untracked rework.
- The machine alone does not make the difference: you need start-of-shift checks, locked recipes, end-of-line checks, structured non-conformity management and reliable records.
- Precision, quality and compliance are linked: when a line loses control over its data, it soon loses margin, traceability and credibility with customers and auditors too.
- Solutions such as electronic paddle graders, combination weighing systems and the Smart combination weigher only deliver real value if they are integrated into clear process standards.
The most dangerous fruit and vegetable packing house mistakes are almost never the spectacular ones. More often they stem from a rushed batch change, a recipe left over from the previous shift, a label that is formally correct but associated with the wrong product, or a weight that is “only slightly over” but across hundreds of cases. That is where the packing house starts to lose margin, time and compliance.
In a fruit and vegetable processing centre, precision and quality do not depend solely on the installed technology, but on the discipline with which flows, settings, checks and records are managed. For the overall picture of operational improvement you can start from the Complete guide to increasing productivity and control in the packing house; here, instead, we focus on high-impact mistakes and how to prevent them in practical terms.
Fruit and vegetable packing house mistakes: where they really originate
The fruit and vegetable packing house is where the product moves from reception, sorting and grading through to packaging, labelling, palletising and shipping. Each stage introduces a different risk: at unloading you can lose batch identity, in grading you can create inconsistent classes, in packaging you can generate giveaway or underweight, and at the end of line you can ship cases with incorrect data.
The problem is that many facilities treat errors as isolated incidents. In reality, they are almost always the result of three systemic causes:
- Unstable flows, with waiting times, build-ups, unnecessary transfers and poorly managed changeovers.
- Weak standards, meaning shift start-ups, recipes, settings and checks that are not always the same across operators and departments.
- Incomplete traceability, with data scattered across paper, terminals, printers, PLCs and operators.
To understand how much these problems weigh on throughput, waste and plant availability, the natural complement is KPIs and OEE for the fruit and vegetable packing house. To reduce the upstream causes, that is, the steps that generate errors and bottlenecks, Optimising flows and layout of the fruit and vegetable line is also useful.
High-impact fruit and vegetable packing house mistakes
Mixed batches: the error that compromises everything
Mixed batches are one of the most serious errors because they simultaneously affect traceability, compliance and the ability to respond in the event of a complaint or recall. They occur when the previous batch is not truly closed, when buffers are not emptied, when cases are left pending at the end of line or when the operator changes product line without formal confirmation.
The typical signs are simple: correct labels that are inconsistent with the product in transit, batch quantities that do not add up, mixed pallets created to make up time. Prevention requires a clear rule: no batch change without an empty line, confirmation in the system and a physical check of the accumulation points.
Incorrect or non-compliant labels
The label is often the last checkpoint and, paradoxically, the most underestimated. An error in the batch, variety, size, nominal weight, country of origin, date or internal code can turn a compliant shipment into a commercial or documentary non-conformity.
Here the error is not just “printing badly”. The real error is allowing printers, recipes, master data and the production order not to speak the same language. That is why it is worth linking label data to a unique recipe and preventing unauthorised free corrections during the shift.
Out-of-tolerance weights: lost margin or risk of complaints
In the packing house, incorrect weight shows up in two opposite ways, both costly:
- underweight, with the risk of complaints, disputes and non-conformities;
- overweight, that is giveaway, which erodes profitability case after case.
On lines equipped with combination weighing systems or the Smart combination weigher, precision can be very high, but only if the product arrives uniformly, the setting is correct and statistical control is continuous. If incoming product is irregular, or if moisture, piece size or fill change without the recipe being updated, the error immediately shifts to the finished case.
Inconsistent grading: unstable perceived quality
When the customer opens two theoretically identical packs and finds product that differs in size, length or class, the problem is almost always inconsistent grading. Having a precise machine is not enough: you need a clear definition of the classes and periodic verification of the actual result.
Bulltec electronic paddle graders are designed for accurate sorting and gentle handling; for some configurations they state a precision of up to ±3 mm for size and high operational continuity. But even precise technology loses effectiveness if the feed is irregular, parameters are not locked or sample checks are not compared with the set classes.
Invisible rework and waste
Rework is often treated as operational normality: you reopen, correct, reprocess and restart. The problem is that, if it is not measured, it hides the real causes. The same applies to waste: it is not enough to know how many kilos were lost; you need to know where, when, why and on which batch.
If a department frequently reworks packs because of weight, label or size errors, it does not have a problem of distracted operators: it has a problem of standards, data control or flow.
Checks and standards: start-of-shift checks, recipes, sampling and NC management
Start-of-shift check
Shift start-up is the moment that decides whether the line will run under control or spend eight hours chasing anomalies. A good start-up check must confirm at least:
- correct batch and product line;
- printers and labels active with the right template;
- recipe selected and locked;
- tare, target weight and tolerances confirmed;
- hygiene status of the line;
- no residues from the previous batch;
- forms or terminals available for quality records.
When these checks are left to individual experience, errors become “random”. When they are standardised, they become preventable.
Recipes and settings: less freedom, more stability
In many packing houses the problem is not a lack of technology, but too much operational freedom. If every shift supervisor changes parameters, thresholds or speeds out of habit, the line loses repeatability.
The useful rule is simple: standard recipes by product, format and customer, with versioning, authorisations and change history. This applies to grading, weight, labels, conveying speed, buffer logic and reject checks. In case of doubt or with complex lines, the support of consultancy and support services helps turn a well-installed machine into a truly stable process.
Quality sampling and end-of-line checks
Effective sampling must not be bureaucratic, but diagnostic. For each product line you should verify at a defined frequency:
- conformity of the actual size with the class;
- average net weight and spread;
- label correctness;
- packaging integrity;
- cleanliness of the case and absence of visible foreign bodies;
- consistency between pallets, cases and documentation.
The end-of-line check is the last barrier before the error leaves the facility. Skipping it during production peaks is a false economy.
Non-conformity management
A well-managed NC does not stop at separating the product. It must answer four questions:
- What exactly is the problem?
- Which batch, machine, shift and order are involved?
- What quantity is at risk?
- What action prevents recurrence?
Without this discipline, the same non-conformity returns in different forms. That is why this in-depth article naturally links to Common mistakes in the fruit and vegetable processing centre and how to avoid them: the goal is not to correct faster, but to get things wrong less often.
Hygiene and contamination: procedures, pest management, event traceability and auditability
Hygiene and contamination are not issues separate from productivity. A line that is dirty, damp, poorly cleaned or has areas that are hard to inspect generates stoppages, waste, rework and reputational risk. Typical critical issues include product residues in blind spots, uncontrolled tools, exposed packaging materials, dirty/clean flows that are not separated and weak pest management.
Minimum procedures that make the difference
The most effective practices are often the least spectacular:
- cleaning plan by area, frequency and responsibility;
- pre-operational check before start-up;
- clear segregation between compliant, suspect and rejected product;
- access and clothing control;
- pest management with defined control points;
- immediate management of breakages, product spills and foreign bodies.
What to record and why
To be auditable it is not enough to “do things well”: you need to be able to prove it. It is advisable to record at least:
- incoming batch and outgoing batch;
- active recipe and changes made;
- sample weights and statistical checks;
- label checks and end-of-line verifications;
- cleaning, sanitising and pre-operational checks;
- plant anomalies, stoppages and interventions;
- non-conformities, segregation and product disposition;
- events related to pests, foreign bodies or contamination.
This data is used to reconstruct events during audits, complaints or root cause analysis. It also helps you understand where to invest: in the machine, the layout, training or the control routine.
From correction to prevention: the real step change
A packing house truly improves when it stops chasing errors and starts designing conditions in which errors are hard to make. This means fewer manual settings, more standard recipes, fewer ambiguous steps, more mandatory confirmations, less scattered data and more traceability.
If you want an integrated path, combine this article with KPIs and OEE for the fruit and vegetable packing house, Optimising flows and layout of the fruit and vegetable line and the Complete framework for fruit and vegetable line productivity and control. For an even broader view, you can also refer to the Complete strategy to improve flows, precision and quality in the packing house.
The bottom line is simple: precision, quality and compliance are not achieved at the end of the line. They are built beforehand, in the standard.
FAQ
What are the most costly mistakes in a fruit and vegetable packing house?
The most costly mistakes in a fruit and vegetable packing house are mixed batches, incorrect labels, out-of-tolerance weights, inconsistent grading and untracked rework, because they simultaneously affect margin, traceability, compliance and reliability towards the customer. Their real impact lies not only in the immediate waste, but also in the time lost correcting, segregating, rechecking and reconstructing data during complaints or audits.
How can mixed batches be avoided during production changeovers?
Mixed batches are avoided by enforcing a mandatory production changeover procedure that requires an emptied line, checked buffers, confirmation of batch closure, a physical check of residual cases and activation of the new recipe only after double confirmation. If even one of these steps is skipped, the risk of compromising traceability increases significantly, especially in accumulation and end-of-line areas.
How much does an out-of-tolerance weight affect profitability?
An out-of-tolerance weight has a major impact on profitability because underweight exposes you to complaints and non-conformities, while overweight generates repeated giveaway on every case produced. Even a few grams over target, multiplied by thousands of packs, can turn into a significant financial loss, which is why stable recipes, statistical checks and frequent verification of actual weight are needed.
Which checks should be mandatory at the start of the shift?
At the start of the shift, the following should be mandatory: checking the active batch, verifying the label template, confirming the correct recipe, checking tare and tolerances, inspecting line hygiene and making sure no residues from the previous batch are present. This initial check drastically reduces repetitive errors that would otherwise only emerge mid-shift, when the cost of correcting them is already higher.
What needs to be recorded to be ready for an audit?
To be ready for an audit you need to keep orderly records of incoming and outgoing batches, recipes and changes, weight checks, label verifications, end-of-line checks, cleaning, non-conformities, segregations and interventions carried out on the line. These records serve to demonstrate that the process is under control and make it possible to quickly reconstruct what happened, when it happened and to which product.